
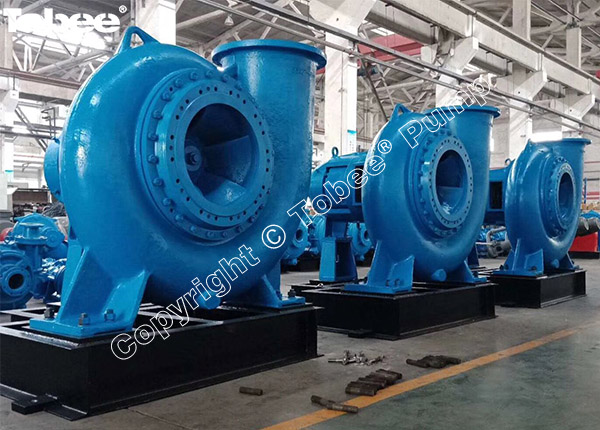


Capacity : 1600 m³/h
Head: 25m
Speed: 960 (r/min)
NPSH: 4.5m
Outlet dia.: 350mm
Inlet dia.: 400mm
The 350X-TL Slurry Pump for FGD Systems by Tobee® is engineered for harsh desulfurization applications in power plants and chemical facilities. As a horizontal FGD pump for limestone slurry transfer, it excels in flue gas desulfurization (FGD) scrubbers, offering high abrasion resistance and unmatched durability. This heavy-duty slurry pump for power plants handles corrosive, abrasive slurries while minimizing downtime. Its corrosion-resistant pump for flue gas desulfurization design ensures longevity in pH 4.5–12 environments.
350X-TL Tobee® FGD Limestone Slurry Pump Performance Parameter:
|
Model |
Capacity Q (m³/h) |
Head H (m) |
Speed n (r/min) |
NPSH (m) |
Outlet dia. (mm) |
Inlet dia. (mm) |
|
350X-TL |
1600 |
25 |
960 |
4.5 |
350 |
400 |
Robust Construction:
• Material: Overflow parts use Tobee®’s proprietary GLH-5/6 alloy, resisting chloride ions up to 20,000 ppm and slurry temperatures ≤65°C.
Performance Efficiency:
Maintenance Advantages:
Applications
|
Industry |
Use Case |
Benefit |
|
Power Plants |
FGD main/circuit slurry transfer |
Handles 60% solids without clogging |
|
Chemical |
Waste slurry cleanup |
GLH-6 alloy resists H₂SO₄ exposure |
|
Oil/Gas |
Byproduct gypsum transport |
20,000+ hr mean time between failures |
Q: Why choose horizontal pumps for FGD systems?
*A: Horizontal designs (like the 350X-TL) simplify maintenance, reduce seal stress, and integrate into tight plant layouts.*
Q: Can this pump handle varying slurry densities?
A: Yes – it operates efficiently at 10–60% Cw concentration and tolerates sudden density shifts.
Q: Are wear parts replaceable onsite?
*A: Absolutely. All wet-end components are modular, cutting downtime by 80% versus welded designs.*
Tobee®’s 350X-TL series combines high abrasion resistance with industry-leading TCO savings:
• Energy Savings: 15% lower kW/ton vs. competitors.• Compliance: Meets ISO 5199/ASME B73.1 standards.
Discover Durable FGD Pumping Solutions!
The 350X-TL Tobee® Limestone Slurry Pump for Desulfurization delivers reliability where others fail. → [Inquire Now for Customized Quotes & Technical Specs!]
 Sara Liang
 +86 189 3110 6396 (Whatsapp/Wechat)
 Inquiry@tobeepump.com
HEBEI TOBEE PUMP CO., LIMITED
Tel: +86 180 3203 4573
Fax: +86 311 8722 1317
E-mail: Sales@tobeepump.com
Skype: Tobee.Pump
Add: No. 266, Tianshan St, High-tech Zone, Shijiazhuang City 050000, China.


