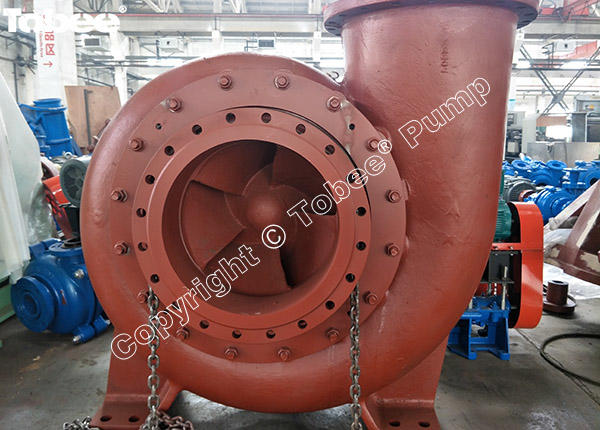
Tobee® 400X-TL FGD Slurry Pump: Power Plant Efficiency & Corrosion Resistance
Optimize your flue gas desulfurization (FGD) performance with the
Tobee® FGD Slurry Pump for Power Plants: the robust 400X-TL Slurry Pump for FGD Applications. Engineered as a horizontal centrifugal pump for slurry handling, it excels as a heavy duty pump for limestone slurry circulation within demanding industrial slurry pump for desulfurization systems. Specifically designed to withstand the harsh, abrasive, and corrosive environments of FGD processes, it delivers unparalleled reliability and corrosion resistant slurry pump for FGD process performance. This horizontal design ensures stable operation and efficient material transport critical for power generation and chemical scrubbing operations.
Key Features & Benefits:
• Superior Corrosion & Wear Resistance: Critical wet end components (impeller, volute liner, suction plate, back plate) utilize specialized alloys engineered for maximum longevity against acidic limestone slurries and aggressive chemicals prevalent in FGD and chemical industry cleaning applications. The suction cover features ductile iron with protective rubber lining.
• Proven Horizontal Design: The stable horizontal centrifugal pump for slurry handling configuration minimizes vibration and noise, ensuring smooth operation and extended mechanical life. Its robust construction handles the demanding heavy duty pump for limestone slurry circulation tasks effortlessly.
• Optimized Hydraulics & Efficiency: Advanced CFD flow simulation guarantees hydraulic efficiency, translating to significant energy savings. The design allows precise impeller positioning adjustment within the casing via the bearing assembly, maintaining peak hydraulic efficiency (Flue Gas Desulfurization Pump with High Efficiency) throughout the impeller's wear life.
• Simplified Maintenance (Back-Pullout): Engineered with a back-pullout structure, maintenance or inspection of seals and bearings is swift. Crucially, this is achieved without disassembling the suction or discharge piping, drastically reducing downtime – essential for continuous industrial slurry pump for desulfurization systems operation.
• Extended Bearing & Seal Life: Robust bearing arrangement features large-capacity tapered roller bearings (drive end) and cylindrical roller bearings (opposite end), lubricated by oil for superior heat dissipation and load handling, significantly enhancing bearing life. The pump integrates specialized mechanical seals designed explicitly for the challenges of FGD slurries, ensuring reliable, leak-free operation.
• Space-Saving & Durable: Features a compact, close-coupled design with an X-type bracket, saving valuable plant floor space while maintaining structural integrity.
Tobee® 400X-TL Flue Gas Desulfurization Slurry Pump Performance Parameter:
|
Model
|
Capacity Q
(m³/h)
|
Head H
(m)
|
Speed n
(r/min)
|
NPSH
(m)
|
Outlet dia.
(mm)
|
Inlet dia.
(mm)
|
|
400X-TL
|
2500
|
25
|
725
|
5.0
|
400
|
450
|
Frequently Asked Questions (FAQ):
Q: Why is the 400X-TL's corrosion resistance critical for FGD?
A: FGD processes involve highly acidic (sulfuric acid) and abrasive limestone/gypsum slurries. The corrosion resistant slurry pump for FGD process construction, using specialized alloys and linings, is essential to prevent rapid deterioration and ensure long service life in this harsh environment.
Q: How does the back-pullout design benefit maintenance?
A: The back-pullout structure allows mechanics to access key components like the impeller, shaft sleeve, and mechanical seal by simply detaching the rear bearing housing without disturbing the pump casing or connected pipelines. This drastically simplifies maintenance and reduces downtime.
Q: Is the 400X-TL suitable beyond power plant FGD?
A: Absolutely. While ideal as a Tobee® FGD Slurry Pump for Power Plants, its robust corrosion resistant design makes it highly effective for chemical processing (acid/alkali transfer, pigment slurries), mining/metallurgy (abrasive ore slurries, electrolytes), wastewater treatment, and any application requiring reliable handling of corrosive or abrasive slurries.
Applications Include:
Power Plant FGD: Limestone Slurry Circulation, Gypsum Slurry, Absorber Tower Recirculation.
Chemical Industry: Acid Transfer (Sulfuric, Hydrochloric), Alkaline Liquids, Corrosive Slurries, Pigment Production, Process Water/Wastewater.
Mining & Metallurgy: Abrasive Ore Slurries, Leaching Solutions, Electrolytes, Tailings.
Wastewater Treatment: Sludge Transfer, Corrosive Effluent Handling.
Boost your FGD system's reliability and efficiency! The Tobee® 400X-TL Slurry Pump for FGD Applications delivers the high efficiency, corrosion resistance, and heavy-duty performance power plants and chemical facilities demand. Contact Tobee® today for expert advice and a quote on the ideal solution for your slurry handling challenges!
 Sara Liang
 +86 189 3110 6396 (Whatsapp/Wechat)
 Inquiry@tobeepump.com