
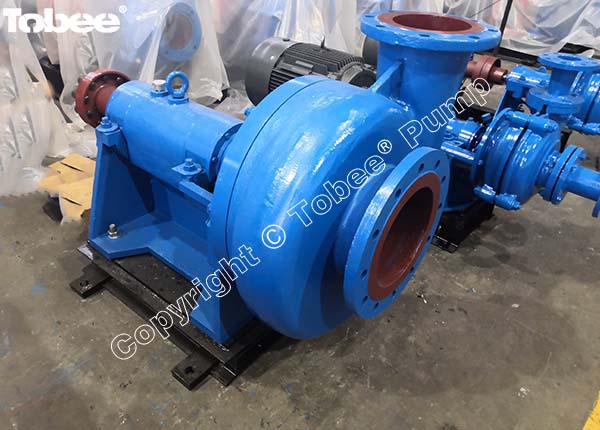


Capacity : 3750 m³/h
Head: 25m
Speed: 725 (r/min)
NPSH: 5.0 m
Outlet dia.: 500mm
Inlet dia.: 500mm
Struggling with abrasive slurry wear, chloride corrosion, or cavitation in your wet desulfurization system? The 500X-TL Slurry Pump for Limestone Slurry by Tobee® delivers unmatched durability for flue gas treatment. Engineered as a Horizontal Centrifugal Pump for FGD Process, it handles aggressive pH 4–6 slurries with >20,000 mg/L chlorides and 15–30% solids. This Abrasion Resistant Pump for Wet Scrubber Use ensures 24/7 operation in power plants and chemical facilities, where efficient pollutant removal is non-negotiable.
Wetted parts use high-chrome alloys (Cr30) or elastomer linings, combating abrasive limestone particles and acidic chloride corrosion. Dual-case construction prevents leakage, extending service life by 40% versus standard pumps.
3. Smart Maintenance Features
• Rear Pull-Out Design: Rotor assembly removal without pipe disassembly.• Robust Shaft & Seal System: Tungsten carbide mechanical seals and oversized bearings resist slurry ingress, reducing downtime.
Model
Capacity Q
(m³/h)
Head H
(m)
Speed n
(r/min)
NPSH
(m)
Outlet dia.
(mm)
Inlet dia.
(mm)
500X-TL
3750
25
725
5.0
500
500
Critical for Chemical Industry Flue Gas Scrubbing
Beyond power plants, this Industrial Slurry Pump for Pollution Control excels in chemical manufacturing, where chloride-rich byproducts accelerate corrosion. Its horizontal configuration simplifies installation in space-constrained scrubber units, while leak-free operation meets environmental compliance.
The 500X-TL Tobee® FGD Pump for Desulfurization Systems ensures reliable limestone slurry transfer in power plant and chemical scrubbers. Choose Tobee® for efficient FGD solutions—Get a Quote Today!
 Sara Liang
 +86 189 3110 6396 (Whatsapp/Wechat)
 Inquiry@tobeepump.com
HEBEI TOBEE PUMP CO., LIMITED
Tel: +86 180 3203 4573
Fax: +86 311 8722 1317
E-mail: Sales@tobeepump.com
Skype: Tobee.Pump
Add: No. 266, Tianshan St, High-tech Zone, Shijiazhuang City 050000, China.


